CPCB & NGT Compliant / Turnkey EPC Engineering / Since 1999
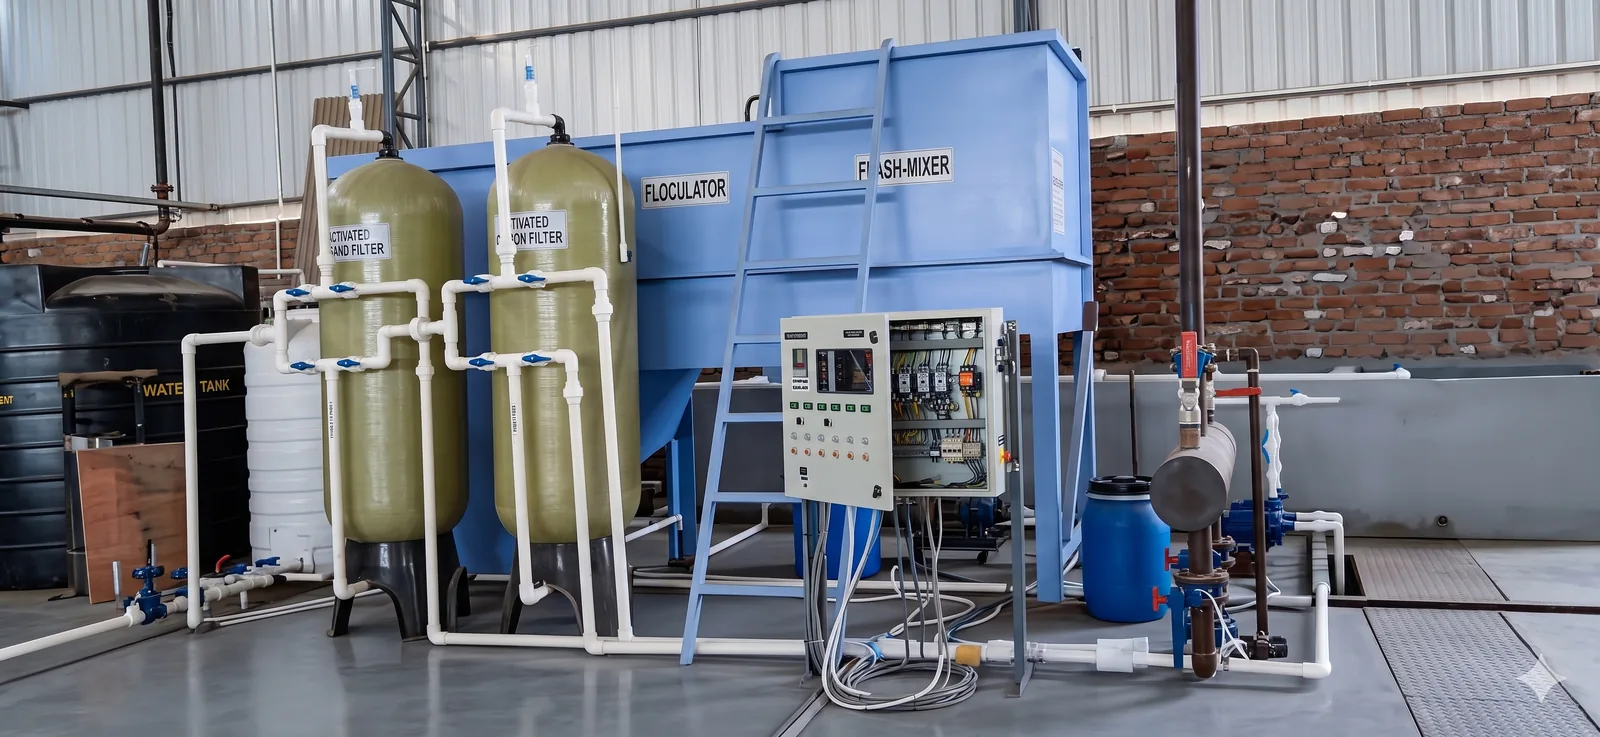
Designing, manufacturing, and commissioning high-capacity industrial Effluent Treatment Plants (ETP), packaged MBR/MBBR Sewage Treatment (STP), and low-energy MVR Zero Liquid Discharge (ZLD) systems.
Turnkey industrial ETP, STP & ZLD plants installed worldwide
Evaporator Uptime recorded across continuous 24/7 operating cycles
Ultra-low Specific Power Consumption index achieved with High-Recovery RO
Guaranteed Compliance with CPCB, SPCB & NGT Zero Liquid Discharge mandates
Explore our range of purpose-engineered wastewater treatment systems designed for heavy industrial COD/BOD loads and zero discharge compliance.
Engineered for severe industrial wastewater streams containing high COD, recalcitrant organic solvents, heavy metals, oil & grease, and complex dye matrices. Features advanced electro-coagulation, Fenton oxidation, and multi-stage biological clarification.
Packaged and civil sewage treatment plants incorporating submerged Flat Sheet or Hollow Fiber Membrane Bioreactors (MBR) and Moving Bed Biofilm Reactors (MBBR). Delivers crystal clear permeate suitable for flush reuse, cooling tower makeup, and landscaping.
Integrated high-recovery Reverse Osmosis, Nanofiltration salt-splitting, and thermal evaporator loops that convert 100% of liquid effluent into high-purity distilled water and solid dry salt cakes for industrial reuse or chemical sale.
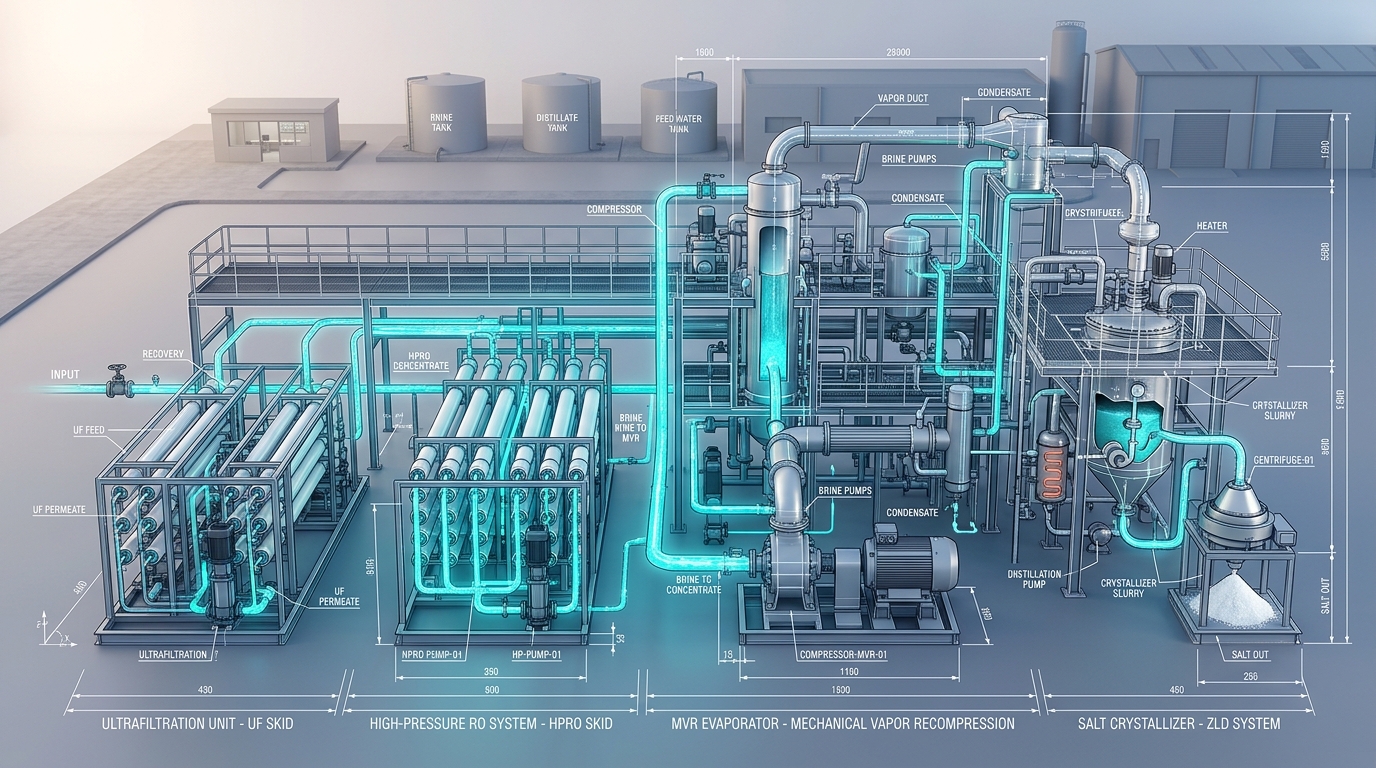
Utilizing high-speed centrifugal vapor compressors to compress secondary steam, recycling latent heat energy into the falling film heat exchanger. Reduces thermal steam requirements by up to 90% compared to traditional Multi-Effect Evaporators (MEE).
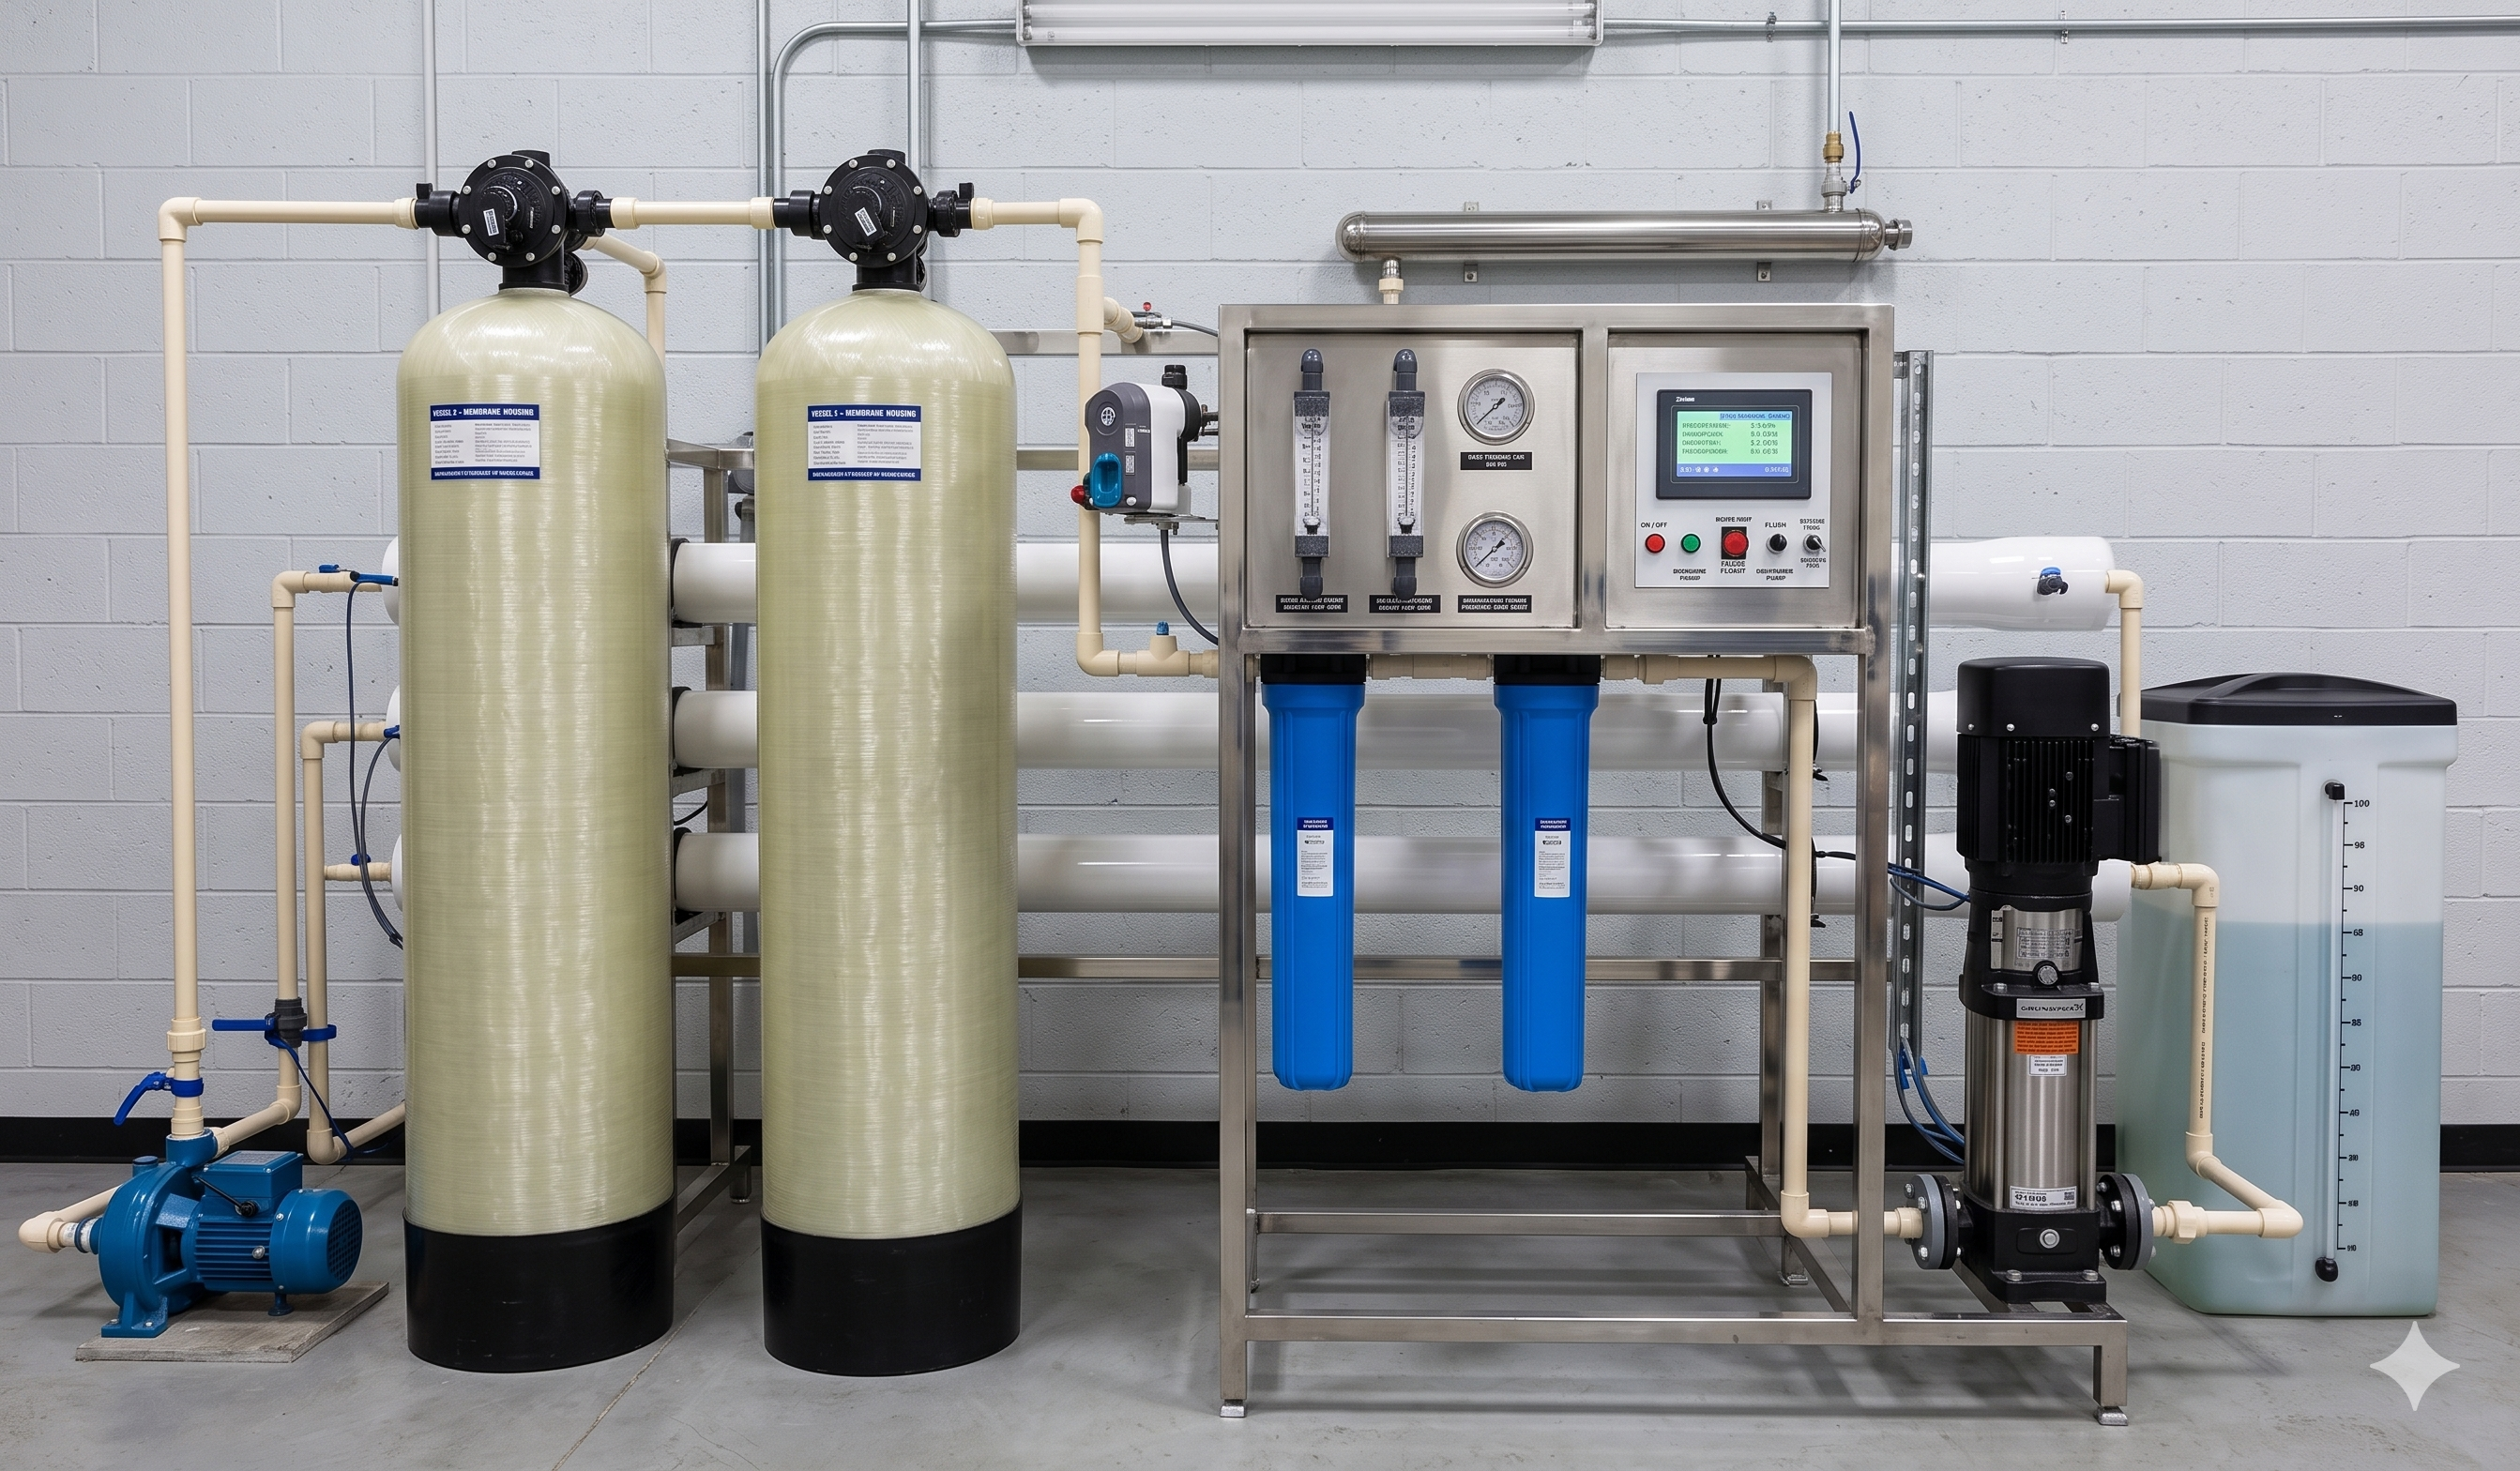
From raw industrial effluent balancing to dry salt crystallization — click each stage to inspect the technical process parameters.
Raw industrial effluent passes through automatic fine bar screens into an agitated equalization basin to buffer peak organic surges. High-speed DAF systems inject micro-bubbles to float emulsified oils, suspended solids, and heavy metals prior to biological treatment.
Core technical advantages engineered into every Rispri Labs water treatment plant.
Destroys toxic recalcitrant molecules, complex aromatics, and refractory pesticides before bio-treatment, enabling clean bacterial degradation.
High chemical resistance and anti-fouling pore geometry. Operates at elevated MLSS (10,000–12,000 mg/L) with zero biomass carryover.
Eliminates boiler steam dependency during continuous evaporation.
Selective nanofiltration salt splitting for marketable industrial salt cake.
Direct real-time streaming of flow, pH, COD, TOC, and TSS data to CPCB server.
Every plant engineered by Rispri Labs is guaranteed to pass stringent Central Pollution Control Board (CPCB) and NGT regulatory inspections. We back our design with comprehensive NABL lab analytical reports and performance test runs.
Compare technical parameters, footprint, energy indices, and effluent treatment capabilities across different system configurations.
| Feature / Metric | Conventional ASP ETP | MBR Packaged STP | High-Recovery ZLD Plant |
|---|---|---|---|
| Water Recovery Rate | 60% – 70% | 85% – 90% | 99.5% – 100% |
| Permeate Quality (BOD / TSS) | BOD < 30, TSS < 50 mg/L | BOD < 5, TSS < 1 mg/L | Distilled Quality (TDS < 50 ppm) |
| Footprint Requirement | 100% (Baseline) | 30% (70% Footprint Saving) | 45% (Includes Evaporator Skid) |
| Specific Power Index | 0.6 – 0.9 kWh/m³ | 0.8 – 1.2 kWh/m³ | 12 – 35 kWh/m³ (MVR Dependent) |
| CPCB Regulatory Compliance | Standard Discharge Limits | Urban Reuse Approved | Zero Discharge Certified |
From initial treatability study to final commercial performance guarantee handover.
Comprehensive analytical testing of raw effluent samples at NABL lab to establish exact BOD, COD, TDS, silica, and organic fraction profiles.
Mass & heat balance simulation, P&ID generation, structural civil layout, 3D piping routing, and electrical control panel architecture.
Precision fabrication of SS316L / Titanium MVR heat exchangers, RO skid assembly, MBR membrane frame assembly, and factory hydro-testing.
Civil integration, electro-mechanical piping installation, SCADA PLC programming, sensor calibration, and dry/wet loop testing.
Continuous 72-hour trial run, NABL permeate testing verification, CPCB OCEMS telemetry connection, and operator training handover.
Clear answers regarding turnkey plant commissioning, CPCB compliance, and operational costs.
Schedule a technical consultation with our senior water treatment engineers or request an NABL treatability audit for your factory effluent.